The vacuum systems in the mining and construction industries are long-term exposed to environments with high dust, high humidity, and heavy-duty continuous operation. Traditional oil-lubricated vacuum pumps are prone to wear and oil circuit blockage after dust intrusion, resulting in frequent maintenance and high downtime costs. Targeting harsh working conditions, Leynow has launched combination solutions of water ring vacuum pumps, Roots vacuum units, and oil-free vacuum pumps, providing a stable and reliable vacuum acquisition method for mining and construction processes ranging from gas drainage and slurry dewatering to pneumatic conveying and foundation treatment.
Challenges Faced by the Industry
The vacuum systems at mining and construction sites face not only the question of "whether it can pump", but more importantly, wear resistance, dust resistance, and continuous stability. In actual projects, customers often encounter the following types of problems:
Dust Intrusion and Wear
High dust concentration in mining crushing, screening, and conveying processes. After dust enters the pump chamber, it accelerates the wear of the rotor and seals, shortening equipment lifespan.
Heavy-duty Continuous Operation
Processes such as gas drainage and slurry filtration require equipment to operate continuously for 24 hours. Pump body overheating and vacuum degree attenuation will directly affect the production pace.
High Pumping Speed and Vacuum Fluctuations
Drainage and filtration processes require continuous high pumping speeds. Vacuum degree fluctuations when pipeline network resistance changes will reduce filtration efficiency and drainage effects.
Maintenance Costs and Downtime Losses
The on-site environment is remote, and spare parts supply and maintenance response are slow. A single unplanned downtime may cause the entire production line to stagnate.
Leynow Mining and Construction Industry Solutions
Targeting the actual working conditions of mines and construction sites, Leynow provides overall vacuum solutions centered on water ring vacuum pumps and Roots vacuum units, forming a complete service closed loop from equipment selection and pipeline design to post-maintenance.
Dust-resistant and Harsh Condition-resistant Design
Water ring vacuum pumps use water as the working fluid and can withstand dust-containing gases and condensable gases. The gap between the impeller and pump body is reasonably designed to reduce dust wear; dust removal and filtration devices can be optionally configured at the front end to further protect the pump body.
Selection Solutions Matched to Working Conditions
Based on pumping volume, vacuum degree range, medium temperature, and dust content, professional engineers provide combination selection of water ring pumps, Roots pumps, or vacuum units, avoiding "using a large pump for a small job" or overload operation.
Guarantee of Stable and Continuous Operation
For long-term continuous operation scenarios such as gas drainage and slurry filtration, the impeller structure and working fluid circulation system are optimized to reduce the risk of pump body overheating and maintain stable vacuum degree output.
Full-cycle Service and Parts Guarantee
Providing installation and commissioning, regular follow-up visits, and maintenance contract services. Repair parts are Leynow original genuine parts. All repair projects come with a 12-month warranty to reduce unplanned downtime.
Core Configured Equipment
According to different mining and construction application scenarios, the following core equipment can be flexibly configured:
| Application Process | Recommended Equipment | Main Function |
|---|---|---|
| Mine Gas Drainage | Water Ring Vacuum Pump / Roots Vacuum Unit | High pumping speed gas drainage, ensuring underground operation safety |
| Slurry Dewatering Filtration | Water Ring Vacuum Pump | Provide stable vacuum for ceramic filters and disc filters |
| Powder Pneumatic Conveying | Roots Vacuum Pump / Vacuum Unit | Convey bulk materials such as cement, mineral powder, and fly ash |
| Soft Foundation Vacuum Preloading | Vacuum Unit / Water Ring Vacuum Pump | Reinforce soft soil foundations, accelerating foundation consolidation and settlement |
| Concrete Vacuum Dewatering | Oil-free Vacuum Pump | Improve concrete compactness and early strength |
| Vacuum Adsorption Hoisting | Oil-free Vacuum Pump / Vacuum Unit | Handling of glass curtain walls, panels, and prefabricated components |
Typical Application Scenarios
Leynow vacuum pumps have been widely used in multiple key processes of the mining and construction industries:
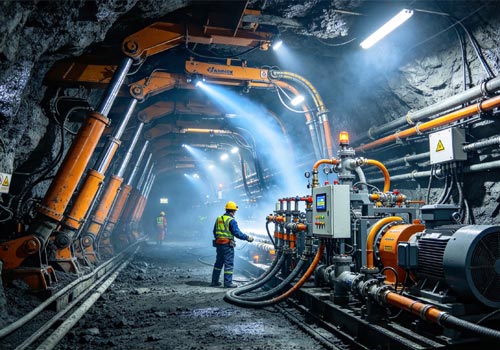
Mine Gas Drainage
Provide high pumping speed vacuum for underground gas drainage systems, ensuring drainage concentration and operation safety.
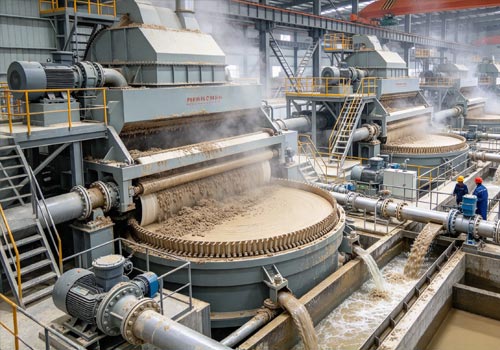
Slurry Dewatering Filtration
Used in the vacuum systems of ceramic filters and disc filters, improving the control effect of filter cake moisture content.
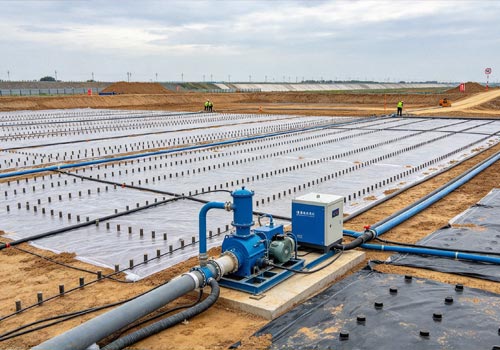
Soft Foundation Vacuum Preloading
Provide continuous and stable negative pressure for foundation treatment, accelerating consolidation and settlement of soft soil foundations.
What Customers Can Gain
Choosing Leynow mining and construction industry vacuum solutions, customers can achieve practical improvements from the following dimensions:
Wear and Dust Resistant
Adapt to dusty and high-humidity working conditions, reducing equipment wear and failures
High Pumping Speed and Stable
Stable vacuum degree output, meeting continuous heavy-duty production needs
Cost Optimization
Reduce consumables and maintenance frequency, decreasing unplanned downtime losses
Service Response
24/7 fault support, on-site service can be arranged in the Pearl River Delta region