Taking stock of common pain points in vacuum applications, providing targeted solutions for selection and operation and maintenance problems.
Ordinary oil-lubricated vacuum pumps discharge oil mist, contaminating materials, food, and electronic workpieces, making the workshop air greasy and increasing environmental treatment costs.
Wrong pump selection, insufficient pumping speed, vacuum degree cannot go up, vacuum drying, defoaming, and coating processes fail to meet standards, and the defective rate of finished products remains high.
Inferior vanes and seals wear quickly, frequent shutdowns for maintenance, difficult procurement of parts, and delays in the normal production progress of the production line.
Not knowing when to use oil-lubricated and when to choose oil-free; buying the wrong model means the equipment cannot match the process, resulting in a waste of procurement funds.
Industrial-grade rotary vane vacuum pump, stable and durable, suitable for diverse vacuum working conditions.
Mature rotary vane structure design, high-strength pump body shell, high-performance vanes, capable of long-term continuous operation, withstanding the harsh working conditions of industrial sites.
Matched with high-efficiency motors, optimized pump chamber structure, reduced operating power consumption, excellent noise control of the whole machine, suitable for long-term use in workshops and laboratories.
Simple structure, easy disassembly and assembly of wearing parts; oil-lubricated pumps can be equipped with exhaust filters, which can filter 99% of oil mist; oil-free models require no vacuum pump oil.
Full series of single-stage oil-lubricated rotary vane, two-stage oil-lubricated rotary vane, and oil-free rotary vane; from rough vacuum to high vacuum, both oil-lubricated and clean oil-free solutions are available.
Can be used as a backing pump for Roots pumps and molecular pumps to form complete vacuum units, meeting the requirements of higher vacuum systems.
Provide selection, installation guidance, and troubleshooting; supply of original factory parts such as vanes, exhaust filters, and seals; support repair and maintenance services.
Oil-sealed mechanical vacuum pump, working pressure 101325 ~ 1.33×10⁻² Pa
High cost-effectiveness, low noise, convenient maintenance, suitable for rough-medium vacuum working conditions
Optional exhaust filter, filtering the vast majority of oil mist emissions
Representative models: LV0020, LV0100, LV0305
Suitable for packaging, metallurgy, chemical, solar energy, and general industrial vacuum pumping
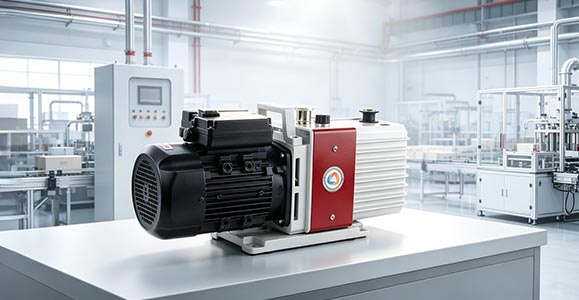
Two-stage series compression for higher ultimate vacuum, up to 0.005mbar
Excellent pumping performance, stronger water vapor tolerance
Suitable for processes and laboratory scenarios with high vacuum requirements
Representative models: LD0016, LD0030
Vacuum coating, freeze-drying, rectification, scientific research experiments, automotive refrigeration industry
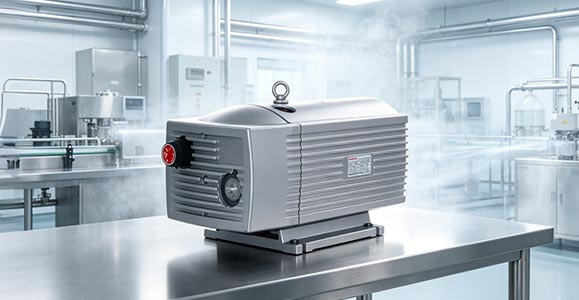
Graphite vane dry structure, no vacuum pump oil required, no risk of oil mist contamination
Outputs clean gas, protecting materials from oil and gas contamination
Representative models: LX0025 H06, LT0010V, LT0025V, LT0060V
Suitable for food, medicine, transportation, power generation, and processes with zero tolerance for oil and gas
Note: Graphite vanes will produce a small amount of graphite dust; add a front-end filtration device if necessary
Specifications overview of the oil-free vacuum pump series for quick matching and selection.
| Product Model | Motor Power | Ultimate Vacuum | Rated Voltage | Rated Current | Rated Flow | Product Category |
|---|---|---|---|---|---|---|
LV 0020 |
0.75 Kw | 0.5 mBar | 200-240△/345-415Y | 2.4 A | 20 m3/h | Single-stage Rotary Vacuum Pump |
LV 0100 |
3.0 Kw | 0.5 mBar | 200-240△/345-415Y | 6.8 A | 100 m3/h | Single-stage Rotary Vacuum Pump |
LV 0305 |
7.5 Kw | 0.1 mBar | 345-415△/600-720Y | 16.7 A | 250 m3/h | Single-stage Rotary Vacuum Pump |
| Comparison Item | Oil-lubricated Rotary Vane Vacuum Pump (Single/Two-stage) | Oil-free Rotary Vane Vacuum Pump |
|---|---|---|
| Working Medium | Requires vacuum pump oil, relies on oil sealing and lubrication | No pump oil required, graphite vanes for solid self-lubrication |
| Ultimate Vacuum | Extremely high, two-stage can reach 0.005mbar | Rough vacuum range, ultimate vacuum is relatively low |
| Contamination Risk | Oil mist exists, exhaust filter can be installed to reduce emissions | No oil mist; produces a small amount of graphite dust, filtration can be added if needed |
| Maintenance Focus | Regular replacement of vacuum pump oil and oil filter | Regular inspection and replacement of graphite vanes |
| Recommended Usage Scenarios | Requires high vacuum, materials are not afraid of trace oil mist; laboratories, coating, drying, distillation | Strictly prohibits oil contamination; food, medicine, some transport and power generation processes |
| Not Recommended Working Conditions | Process media strictly prohibited from contacting oil mist | Working conditions pursuing ultra-high ultimate vacuum |
Compiled technical reference materials related to vacuum pumps for selection, equipment commissioning, and troubleshooting.
Covering negative pressure processes in multiple industries, clean rotary vane vacuum solutions are suitable for various scenarios.

Used for vacuum packaging, degassing, and preservation. Oil-free models eliminate oil mist contamination of food, ensuring hygiene and safety.

Processes such as freeze-drying, concentration, and filtration. Oil-free clean vacuum solutions avoid cross-contamination of pharmaceuticals.

Processes such as coating, etching, and packaging. Two-stage oil-lubricated rotary vane pumps provide stable high vacuum, ensuring yield.

Cell coating and lamination vacuum pumping. Oil-lubricated rotary vane vacuum pumps are stable and reliable, suitable for continuous production.

Vacuum melting, annealing, and sintering. Under high-temperature working conditions, oil-lubricated rotary vane pumps maintain stable pumping speed.

Processes such as distillation, desolvation, and drying. Anti-corrosion oil-lubricated rotary vane pumps adapt to a variety of chemical media.

Two-stage oil-lubricated rotary vane pumps have a high ultimate vacuum, meeting the needs of precision experiments such as freeze-drying, coating, and analytical instruments.

Vacuum pumping and leak detection of refrigeration systems. Oil-lubricated rotary vane pumps have fast pumping speeds, shortening the production cycle.

Two-stage oil-lubricated rotary vane pumps are used as backing pumps, combined with Roots pumps or molecular pumps, to obtain a highly clean vacuum environment.

Removing moisture and bubbles from materials. Oil-lubricated rotary vane pumps have stable pumping speed and high drying efficiency.

Accelerating liquid filtration and impregnation penetration. Oil-free models are suitable for clean scenarios in food and medicine.

Lowering the boiling point of materials and preventing the decomposition of heat-sensitive substances. Two-stage oil-lubricated rotary vane pumps provide stable vacuum.

Quickly lowering the temperature of fruits and vegetables and extending the preservation period. Oil-lubricated rotary vane pumps with large pumping speed quickly establish vacuum.

Combining with Roots pumps and molecular pumps to form vacuum units, achieving greater pumping speed and higher ultimate vacuum.

Removing dissolved gases and tiny bubbles in liquids or resins, preventing pore defects, and improving product density and appearance quality.

Using vacuum negative pressure to adsorb workpieces such as glass, panels, and cartons, and cooperating with robotic arms to achieve automated handling and palletizing.
Summary of common questions to help with quick selection.
For ordinary rough-medium vacuum and the pursuit of cost-effectiveness, prioritize single-stage oil-lubricated rotary vane vacuum pumps; if the process requires a very high ultimate vacuum, such as coating, freeze-drying, and precision experiments, prioritize two-stage oil-lubricated rotary vane vacuum pumps.
An original exhaust filter can be configured, which can filter 99% of oil mist; replace the vacuum pump oil regularly, choose food-grade vacuum pump oil, and proper maintenance can greatly reduce oil mist emissions.
Oil-free models do not generate oil mist, but the friction of graphite vanes will produce a small amount of graphite dust; if the process is sensitive to dust, a filtration device needs to be equipped at the intake or exhaust end.
Yes, single-stage and two-stage oil-lubricated rotary vane vacuum pumps are often used as backing pumps for Roots vacuum units. After combination, they achieve greater pumping speed and higher vacuum.
Oil-lubricated rotary vane pumps are not suitable for extracting highly corrosive gases, large amounts of dust particles, or high-concentration oxygen; they cannot be used as transfer pumps or compression pumps; it is recommended to add a pre-treatment device for corrosive gases.
Yes; complete accessories such as vanes, exhaust filters, seals, and vacuum pump oil; provide troubleshooting consultation, factory repair, and on-site maintenance technical guidance.
Please fill in your requirements carefully, and we will contact you within 24 hours.