The production environment of the oil and gas industry has distinct characteristics such as flammability and explosiveness, sulfur-containing corrosion, and continuous heavy-duty operation. Traditional vacuum equipment often has shortcomings in explosion-proof rating, corrosion resistance, and continuous operation stability. Once a leak or spark occurs, the consequences are unbearable. Leynow explosion-proof vacuum pumps and vacuum units adopt explosion-proof motors and corrosion-resistant structural designs, reducing safety risks from the source, and have become the preferred configuration for multiple processes such as oil and gas recovery, natural gas processing, and refining production.
Challenges Faced by the Industry
The requirements of oil and gas production for vacuum systems are not just about "pulling a vacuum", but more importantly, explosion-proof, corrosion-resistant, and continuous and reliable. In practical applications, customers often encounter the following types of problems:
Risk of Flammability and Explosiveness
Accumulation of volatile oil and gas. If ordinary vacuum equipment generates electric sparks or high-temperature surfaces, it may cause serious safety accidents.
Sulfur-containing Acidic Corrosion
Acidic gases such as H2S and CO2 significantly corrode the pump body and seals, leading to vacuum degree attenuation and shortened equipment lifespan.
Continuous Heavy-Duty Operation
Processes such as oil and gas recovery and flare gas recovery require long-term continuous operation. Pump body overheating or vacuum fluctuations will directly affect process effects.
Safety Compliance and Maintenance
The petrochemical industry has clear requirements for equipment explosion-proof certification, maintenance cycles, and operation records. Equipment must be easy to manage and trace.
Leynow Oil and Gas Industry Solutions
Targeting the actual working conditions of the oil, gas, and petrochemical industries, Leynow provides overall vacuum solutions centered on explosion-proof vacuum pumps, forming a complete service closed loop from equipment selection and installation and commissioning to post-maintenance.
Explosion-proof Design, Adaptable to Hazardous Areas
Equipped with explosion-proof motors and explosion-proof junction boxes, the complete machine structure strengthens heat dissipation and sealing, meeting the usage requirements in explosive gas environments and reducing the risk of ignition sources.
Corrosion-resistant Structure and Material Selection
For sulfur-containing, acidic, and humid working conditions, provide corrosion-resistant materials and sealing solutions to slow down the corrosion of the pump chamber and valve components, extending equipment service life.
Selection Solutions Matched to Working Conditions
Based on pumping volume, vacuum degree, gas composition, ambient temperature, and explosion-proof area rating, professional engineers provide selection suggestions to avoid efficiency and lifespan issues caused by selection deviations.
Full-cycle Service and Parts Guarantee
Providing installation and commissioning, regular follow-up visits, and maintenance contract services. Repair parts are Leynow original genuine parts. All repair projects come with a 12-month warranty to reduce unplanned downtime.
Core Configured Equipment
According to different oil, gas, and petrochemical application scenarios, the following core equipment can be flexibly configured:
| Application Process | Recommended Equipment | Main Function |
|---|---|---|
| Oil and Gas Recovery | Explosion-proof Vacuum Pump / Vacuum Unit | Recover volatile oil and gas from storage tanks and loading/unloading trucks, reducing VOCs emissions |
| Natural Gas Dehydration | Liquid Ring Vacuum Pump / Vacuum Unit | Provide stable vacuum for dehydration units, ensuring dehydration effects |
| Vacuum Distillation | Screw Vacuum Pump / Vacuum Unit | Vacuum pumping for refinery vacuum towers, improving separation efficiency |
| Flare Gas Recovery | Explosion-proof Vacuum Pump | Recover flare exhaust gas, reducing energy consumption and emissions |
| Tank Vacuum Pumping | Explosion-proof Vacuum Pump / Vacuum Unit | Tank gas replacement, vacuum pumping, and inerting treatment |
Typical Application Scenarios
Leynow explosion-proof vacuum pumps have been widely used in multiple key processes of the oil and gas industry:
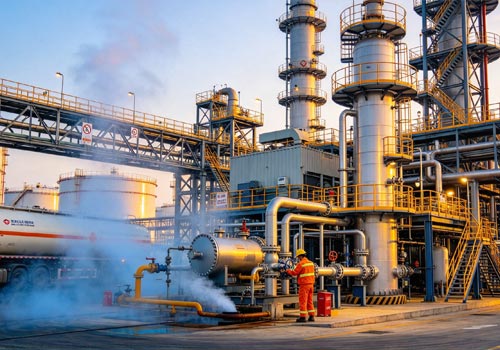
Oil and Gas Recovery
Used in oil and gas recovery systems for storage tanks and loading/unloading trucks. Explosion-proof and reliable, reducing VOCs emissions.
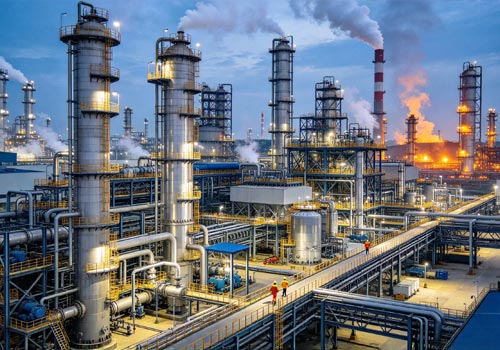
Refining Production
Used in processes such as vacuum distillation, dewaxing, and decolorization, providing stable and continuous vacuum.
Natural Gas Processing
Used in the vacuum systems of natural gas dehydration and desulfurization units. Corrosion-resistant design for greater durability.
What Customers Can Gain
Choosing Leynow oil and gas industry vacuum solutions, customers can achieve practical improvements from the following dimensions:
Explosion-proof Safety
Explosion-proof design, adaptable to usage requirements in hazardous areas
Corrosion-resistant and Durable
Corrosion-resistant structure and materials, handling sulfur-containing acidic gases
Cost Optimization
Reduce unplanned downtime and repairs, lowering overall usage costs
Service Response
24/7 fault support, on-site service can be arranged in the Pearl River Delta region