In petrochemical production processes, vacuum systems are widely used in processes such as vacuum distillation, oil and gas recovery, vacuum degassing, solvent recovery, vacuum drying, and tail gas treatment. These working conditions are often accompanied by flammable and explosive gases, corrosive media, and high-temperature and high-humidity environments, placing strict requirements on the explosion-proof rating, corrosion resistance, and continuous operation stability of vacuum pumps. Targeting the special working conditions of the petrochemical industry, Leynow provides combination solutions of liquid ring vacuum pumps, Roots vacuum pumps, and dry vacuum pumps, forming complete vacuum system service capabilities from selection and explosion-proof configuration to installation and maintenance.
Challenges Faced by the Industry
The requirements of petrochemical plants for vacuum systems are not just about "pulling a vacuum", but more importantly, explosion-proof, corrosion-resistant, and capable of continuous operation. In practical applications, customers often encounter the following types of problems:
Risk of Flammable and Explosive Gases
Petrochemical processes are often accompanied by combustible gases or volatile solvent vapors. Vacuum pumps need explosion-proof configurations to avoid safety accidents caused by electric sparks or high temperatures.
Erosion by Corrosive Media
Corrosive media such as acid gases, hydrogen sulfide, and organic solvents accelerate the aging of the pump body and seals, shortening equipment lifespan and increasing leakage risks.
High-Temperature and High-Humidity Continuous Operation
Refining and chemical plants mostly operate continuously for 24 hours. Under high-temperature and high-humidity conditions, pump body overheating and vacuum fluctuations directly affect distillation and degassing effects.
Maintenance and Compliance Costs
Vacuum pump oil needs to be replaced regularly, and oil-containing exhaust gas needs to be treated. Combined with explosion-proof maintenance and compliance requirements, overall maintenance costs are relatively high.
Leynow Petrochemical Industry Solutions
Targeting the actual working conditions of the petrochemical industry, Leynow provides vacuum system solutions centered on liquid ring vacuum pumps, Roots vacuum pumps, and dry vacuum pumps, forming a complete service closed loop from working condition assessment and explosion-proof configuration to installation and commissioning and post-maintenance.
Explosion-proof Vacuum System Configuration
According to the explosion level of the process medium, provide explosion-proof motors, explosion-proof control cabinets, and electrostatic grounding configurations to meet the usage requirements of explosion-proof areas in petrochemical plants.
Corrosion-resistant Materials and Sealing Solutions
For working conditions with acid gases and organic solvents, optional corrosion-resistant materials such as stainless steel and fluorine-lined materials can be provided, combined with double-end mechanical seals or magnetic seals to reduce leakage risks.
Selection Solutions Matched to Process Parameters
Based on the vacuum degree range, pumping volume, medium temperature, and corrosiveness, professional engineers provide combination selection suggestions for liquid ring pumps, Roots pumps, and dry pumps to avoid efficiency and lifespan issues.
Full-cycle Service and Parts Guarantee
Providing installation and commissioning, regular follow-up visits, and maintenance contract services. Repair parts are Leynow original genuine parts. All repair projects come with a 12-month warranty to reduce unplanned downtime.
Core Configured Equipment
According to different petrochemical process stages, the following core equipment can be flexibly configured:
| Application Process | Recommended Equipment | Main Function |
|---|---|---|
| Vacuum Distillation | Liquid Ring Vacuum Pump / Roots Vacuum Pump | Reduce tower pressure, ensuring distillation separation efficiency and product quality |
| Oil and Gas Recovery | Liquid Ring Vacuum Pump / Dry Vacuum Pump | Recover volatile oil and gas in storage and transportation, reducing losses and emissions |
| Vacuum Degassing | Liquid Ring Vacuum Pump / Vacuum Unit | Remove dissolved gases and moisture from oil products or chemical materials |
| Solvent Recovery | Dry Vacuum Pump / Roots Vacuum Pump | Cooperate with condensation recovery of organic solvents, reducing material loss |
| Vacuum Drying | Liquid Ring Vacuum Pump / Vacuum Unit | Meet the low-temperature drying and vacuum dehydration requirements of chemical materials |
| Tail Gas Treatment | Liquid Ring Vacuum Pump | Extract corrosive tail gas, cooperating with absorption towers for compliant emissions |
Typical Application Scenarios
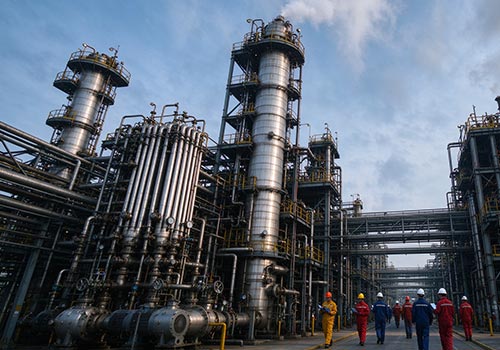
Leynow vacuum systems have been widely used in multiple key processes of the petrochemical industry:
Vacuum Distillation
Provide stable vacuum for refining and chemical distillation towers, ensuring separation efficiency and product quality.
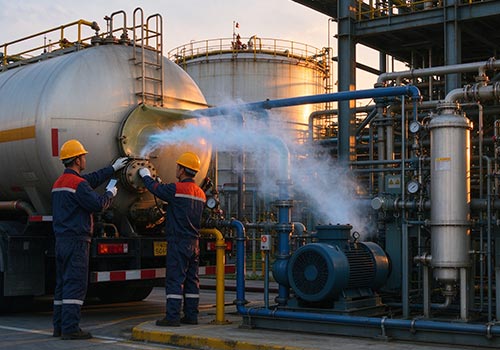
Oil and Gas Recovery
Used for oil and gas recovery units in storage and transportation, reducing volatile organic compound emissions and material loss.
Solvent Recovery
Cooperate with condensation systems to recover organic solvents, reducing production costs and environmental pressure.
What Customers Can Gain
Choosing Leynow petrochemical industry vacuum solutions, customers can achieve practical improvements from the following dimensions:
Safety and Explosion-proof
Explosion-proof configuration and electrostatic grounding, meeting the usage requirements of petrochemical explosion-proof areas
Stable Operation
Stable vacuum degree output, adapting to 24-hour continuous operation conditions
Cost Optimization
Corrosion-resistant materials and reliable seals, reducing maintenance and replacement costs
Service Response
24/7 fault support, on-site service can be arranged in the Pearl River Delta region